English
Contact
Configure
Catalog

Whether you run a manufacturing plant, warehouse, steel facility, power station, or engineering workshop, the quality of your EOT crane directly affects productivity. A well-designed crane can improve workflow, reduce downtime, and support safer material handling across your facility.
This guide will help you understand what separates leading manufacturers from the rest and how to identify the right partner for your lifting requirements.
An Electric Overhead Travelling (EOT) Crane is one of the most widely used material handling systems in industrial environments.
These cranes operate on elevated runway beams and move loads horizontally and vertically throughout a facility. Their ability to transport heavy materials efficiently makes them essential for industries where speed, precision, and safety matter.
EOT cranes help businesses:
Without a reliable crane system, many industrial operations would face significant challenges in daily material handling activities.
The top EOT crane manufacturers in India share several qualities that distinguish them from ordinary equipment suppliers.
Leading manufacturers invest heavily in engineering capabilities.
Their teams understand structural design, load calculations, safety requirements, and industry-specific operational needs.
Modern production facilities allow manufacturers to maintain high quality standards and deliver consistent performance.
No two industrial facilities are exactly alike.
The best manufacturers design cranes based on:
Safety remains one of the most important considerations in crane manufacturing.
Top manufacturers integrate:
The top EOT crane manufacturers in India typically provide a wide range of lifting solutions.
Single girder cranes are commonly used for moderate lifting applications.
Benefits include:
Double girder cranes are designed for heavier loads and demanding applications.
Advantages include:
Many industries require specialized lifting solutions tailored to unique operational requirements.
Leading manufacturers offer custom-designed systems to meet these needs.
A wide range of industries depend on reliable crane systems.
Factories use cranes to transport raw materials, machinery components, and finished products.
Steel production facilities rely on cranes for handling coils, billets, slabs, and structural sections.
Vehicle manufacturing operations require precise movement of large components.
Heavy equipment installation and maintenance often depend on EOT cranes.
Fabrication facilities use cranes to improve efficiency and workplace safety.
Overhead cranes help streamline storage and inventory management processes.
Finding the right manufacturer requires careful evaluation.
A proven track record often reflects reliability and technical expertise.
I've noticed that companies with decades of experience typically have a deeper understanding of industry challenges and customer requirements.
Evaluate the quality of materials, fabrication standards, and engineering processes.
After-sales support plays a major role in long-term crane performance.
Look for manufacturers offering:
Manufacturers should follow recognized engineering and safety guidelines.
Reviewing previous projects provides insight into a manufacturer's capabilities.
When I tried assessing crane suppliers for a large industrial project, project references often revealed more about a company's expertise than brochures or marketing materials.
Working with an established manufacturer provides several long-term advantages.
Well-engineered cranes generally experience fewer operational issues.
Efficient material handling helps maintain smooth production workflows.
Advanced safety systems help reduce operational risks.
Quality construction contributes to long-term durability.
Experienced manufacturers can recommend the most suitable crane solutions for specific applications.
Technology continues to transform crane design and performance.
Real-time monitoring allows operators to track crane performance and identify issues early.
Advanced sensors help detect wear before major failures occur.
Modern systems improve operational efficiency while reducing energy consumption.
Remote operation improves flexibility and enhances workplace safety.
According to an industrial automation study published by a leading engineering research organization, facilities using predictive maintenance technologies have reported significant reductions in equipment downtime and maintenance disruptions.
Many companies focus on immediate requirements without considering long-term needs.
A crane system should accommodate potential growth whenever possible.
Long-term reliability often provides greater value than short-term savings.
Maintenance services play a vital role in crane performance.
Always assess a manufacturer's track record before making a decision.
In my experience, organizations that thoroughly evaluate manufacturer capabilities usually achieve better operational outcomes over the lifespan of the crane.
Times Krane has earned recognition by focusing on quality engineering, customer support, and dependable lifting solutions.
Our expertise includes:
At Times Krane, every project begins with understanding your operational objectives. This helps ensure that the crane system aligns with your production requirements, facility layout, and future growth plans.
I've noticed that the most successful crane projects involve close collaboration between the manufacturer and the customer. That approach remains central to how Times Krane works with businesses across industries.
Whether you need a standard overhead crane or a highly specialized lifting solution, Times Krane focuses on delivering performance, safety, and reliability.
The Indian manufacturing sector continues to expand, increasing demand for advanced material handling solutions.
Future trends include:
Manufacturers that embrace these innovations will continue to lead the industry.
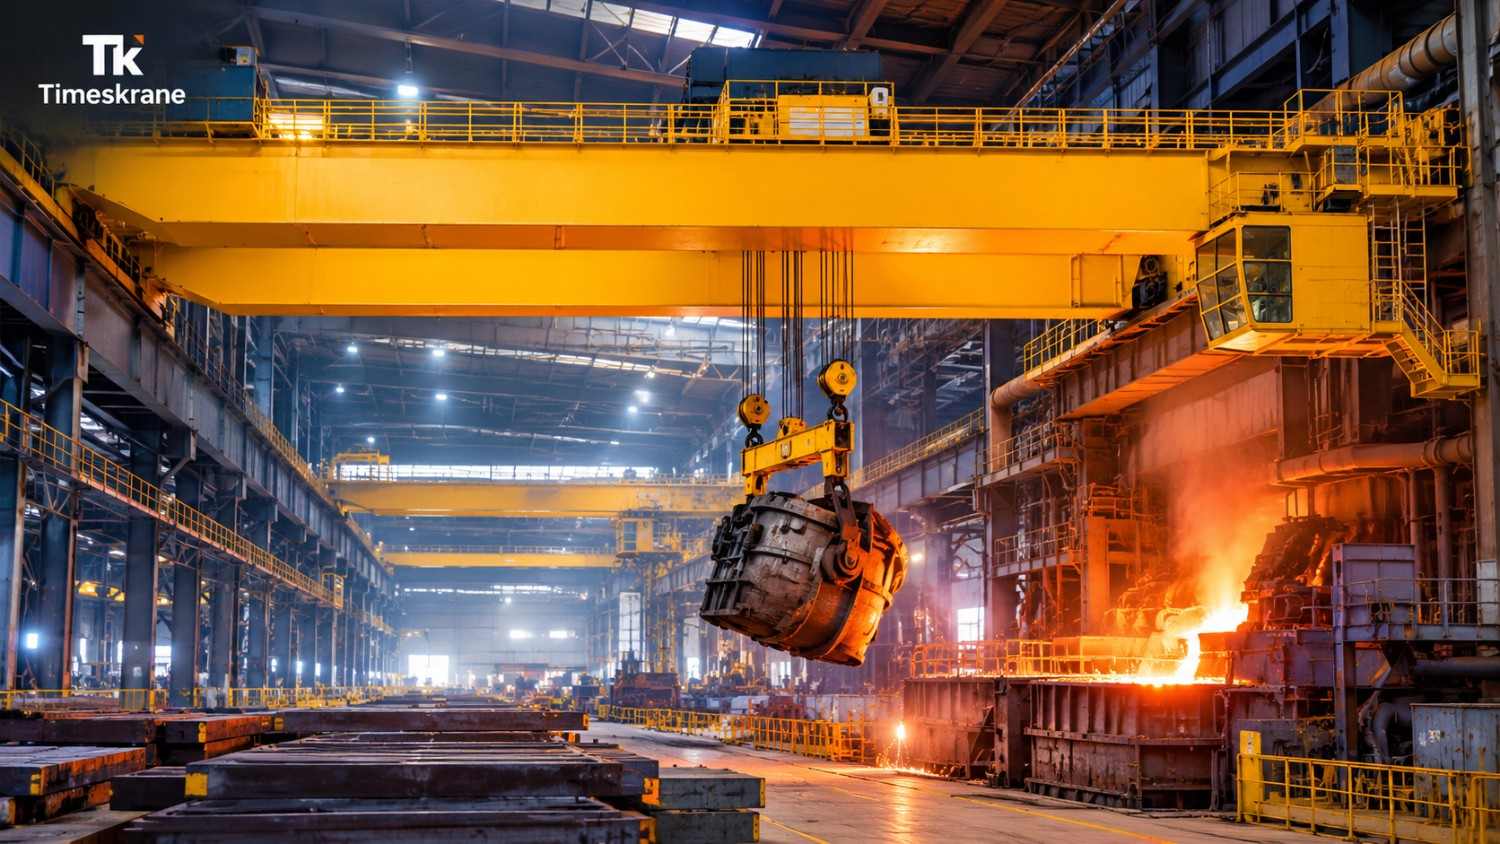
An honest breakdown of what makes a crane genuinely heavy duty for steel plant use, covering duty classification, capacity, and safety features buyers often miss.
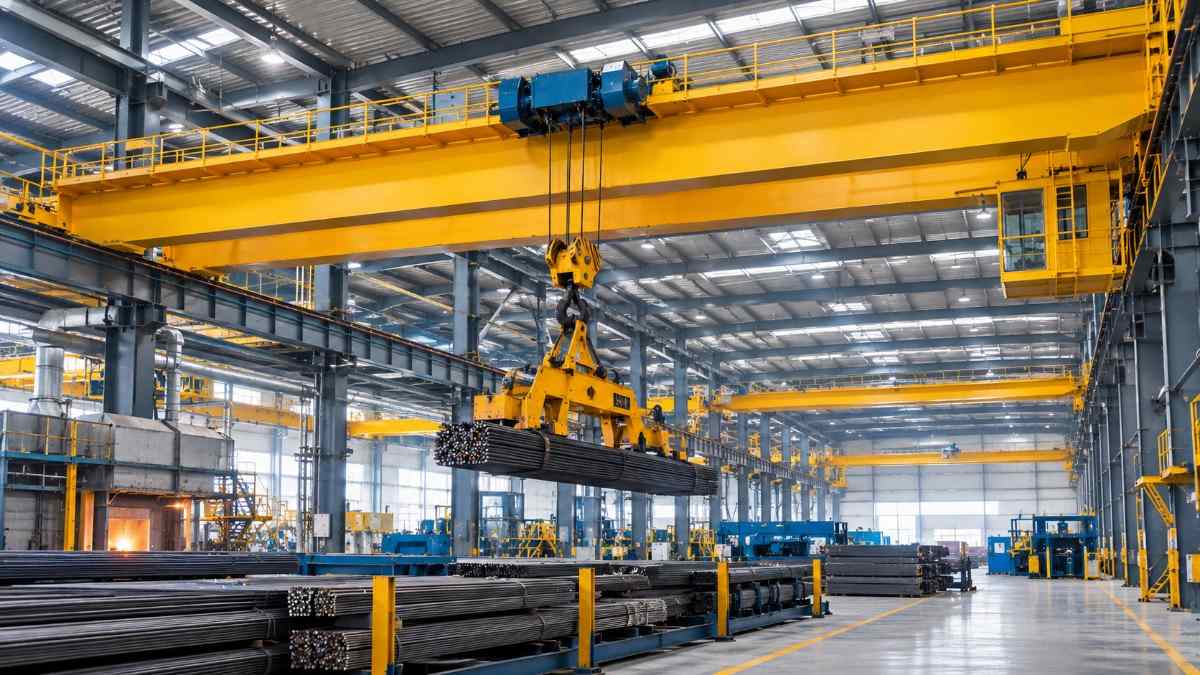
Finding the right steel plant crane manufacturer is perhaps the most important decision a procurement manager or plant owner will make. A poorly designed crane can increase both safety risks and downtime while excessively increasing maintenance costs.
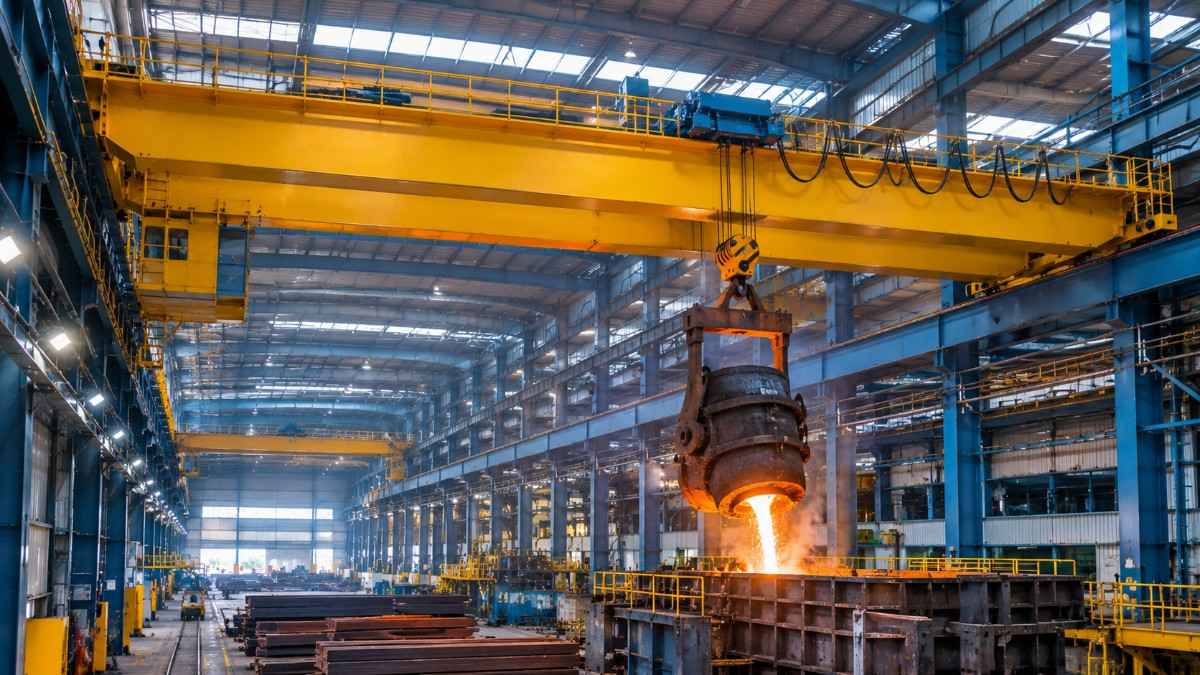
If you run or manage a steel plant, you already know that an overhead crane for steel plant operations is not a luxury. It is the backbone of your material handling process. From moving billets and coils to shifting ladles of molten metal, the right crane decides how smoothly your production line runs.
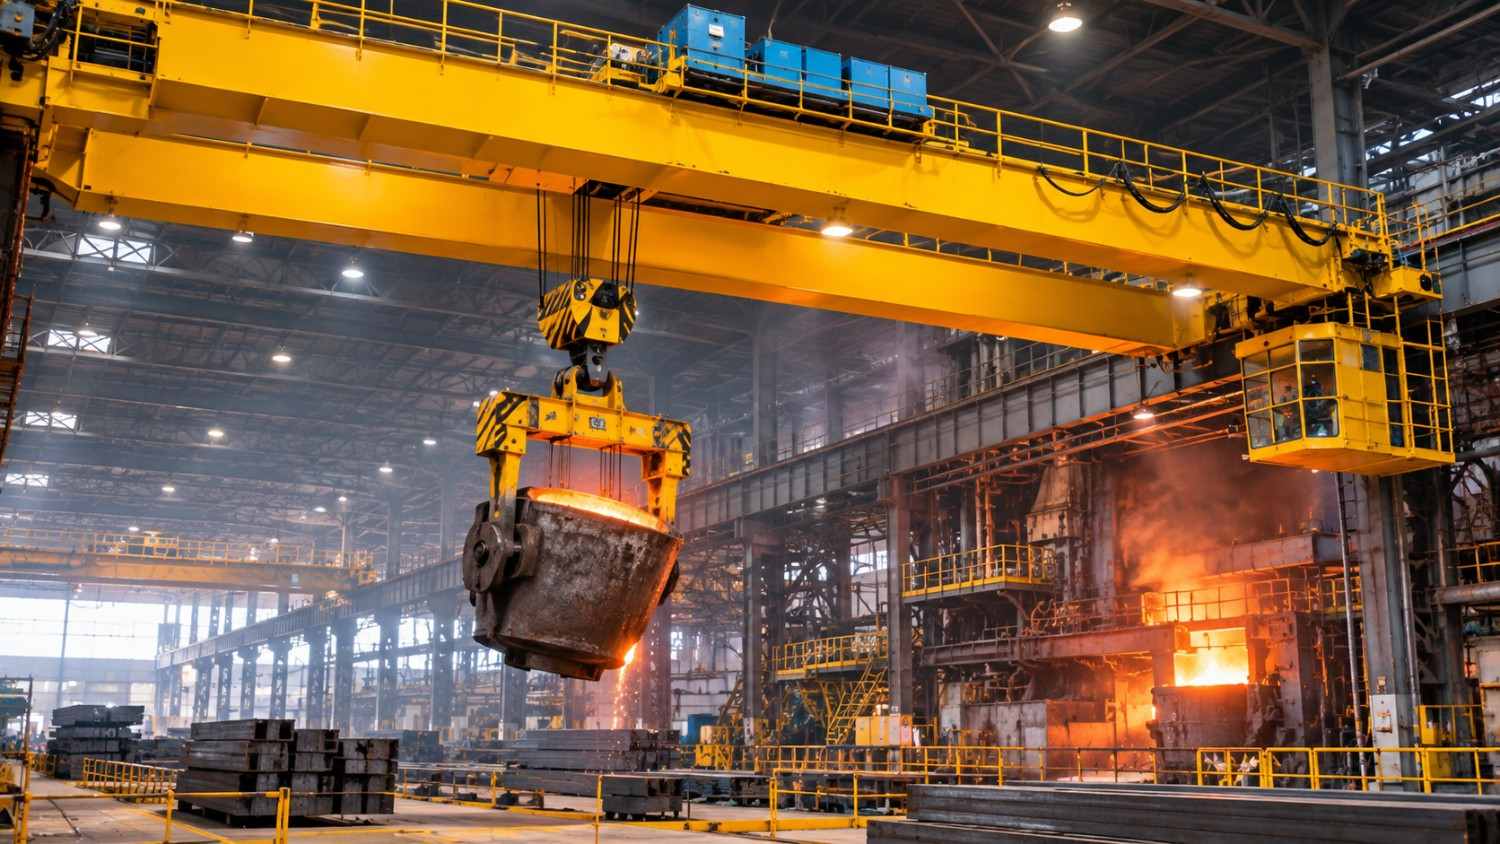
Discover how EOT cranes support steel plant operations, from material handling to molten metal lifting. Learn about crane types, duty classes, safety features, and how to choose the right EOT crane for your steel plant.
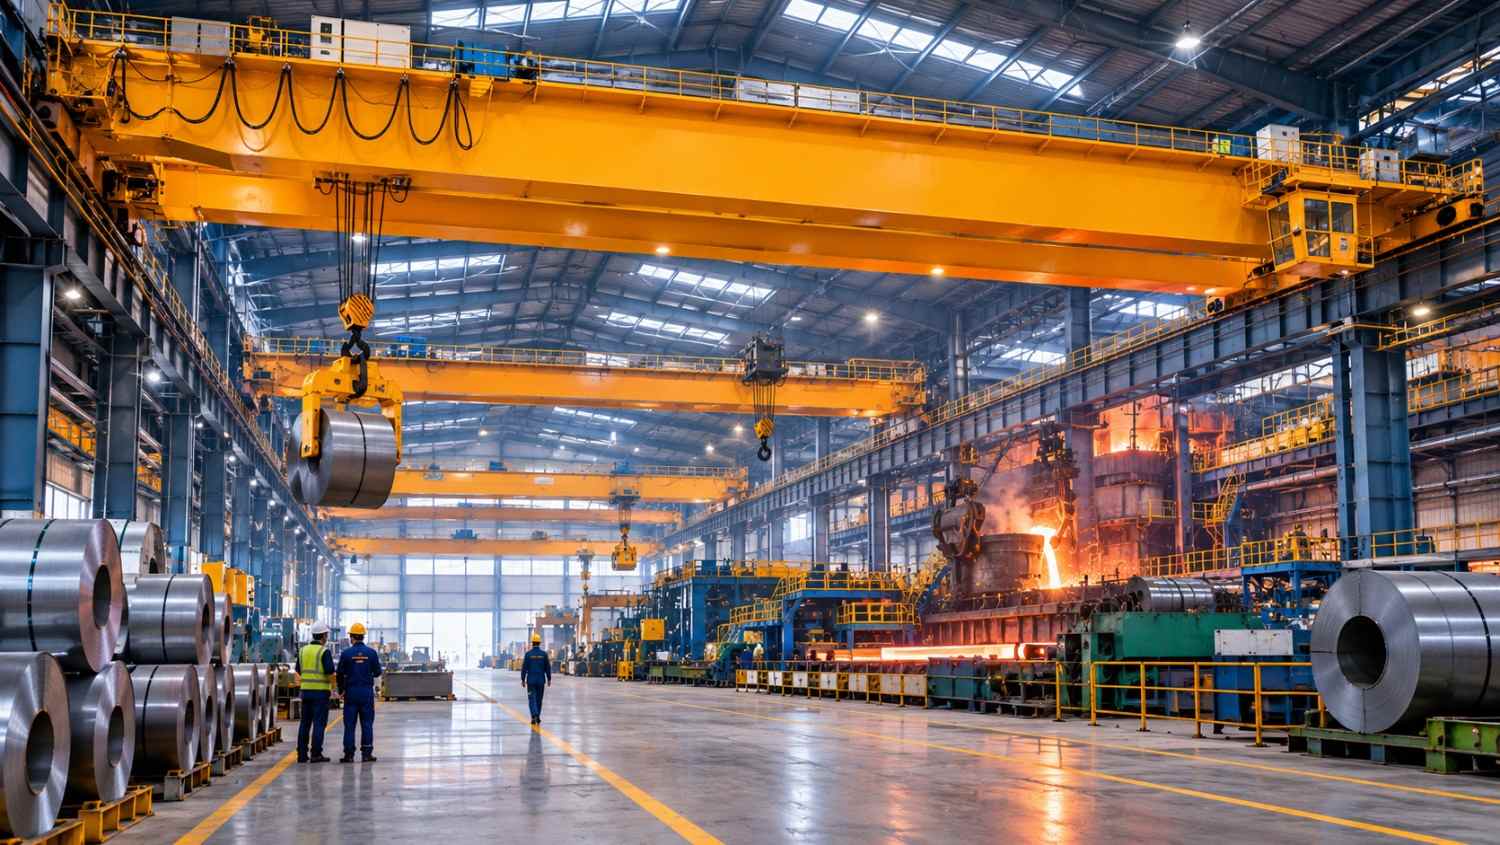
An honest, researched look at the top 5 crane manufacturers for steel plants in India, covering ladle, grab bucket, and coil handling cranes.
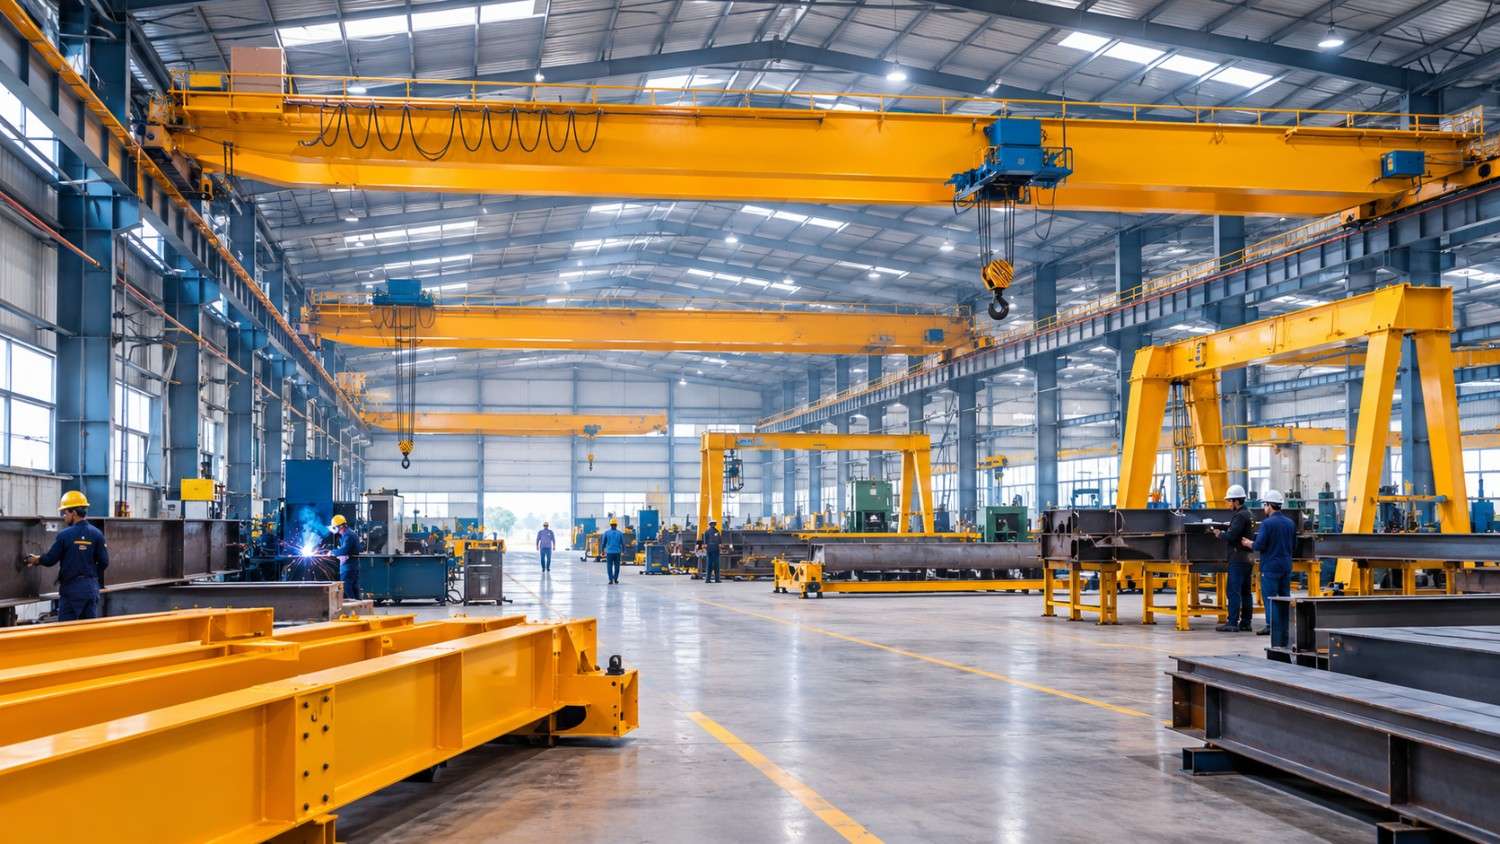
A real, researched look at the top 10 crane manufacturers in North India, covering Delhi NCR, Punjab, Haryana, UP, and Rajasthan, with what actually sets each one apart.
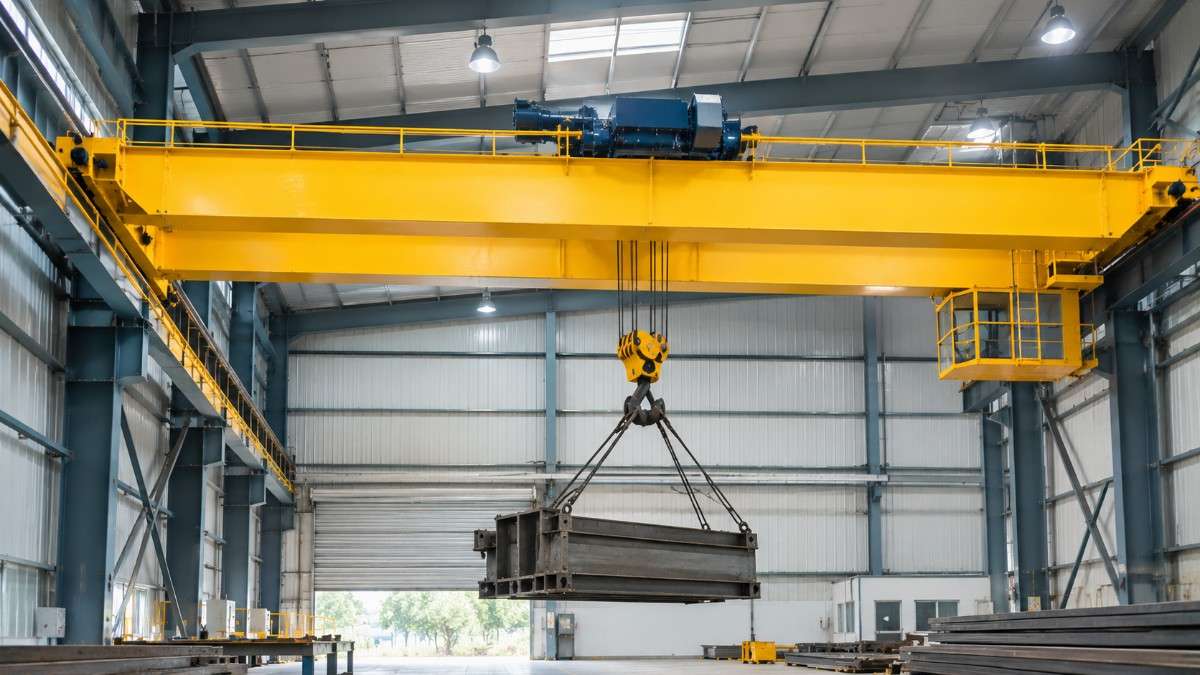
If you are looking for a 10 ton overhead crane for your factory or warehouse, the primary question that arises in your mind is whether this capacity will cater to your daily operations or it will turn out to be a useless and bulky addition to your storage.
Looking for a reliable partner for your next industrial project?