English
Contact
Configure
Catalog
That’s why choosing experienced over head crane manufacturers matters more than many businesses expect.
A well-built overhead crane improves workflow, increases workplace safety, and supports long-term productivity. A poorly engineered one creates maintenance issues, production delays, and operational stress that nobody wants to deal with.
At Times Krane, we’ve worked with industries where dependable lifting systems are part of daily operations, not occasional equipment. The difference between a reliable crane and an unreliable one becomes obvious very quickly on a busy factory floor.
An over head crane is an industrial lifting system installed above the working area to move heavy materials horizontally and vertically.
The crane typically operates using:
Instead of relying entirely on forklifts or manual handling, overhead cranes transport loads efficiently across the facility while keeping floor space clear.
You’ll commonly find these cranes in:
Material handling directly affects production efficiency. When lifting systems slow down, every connected operation feels the impact.
I’ve noticed that businesses upgrading from outdated handling methods often experience smoother workflow almost immediately after installing properly designed crane systems.
Reliable over head crane manufacturers help industries by providing:
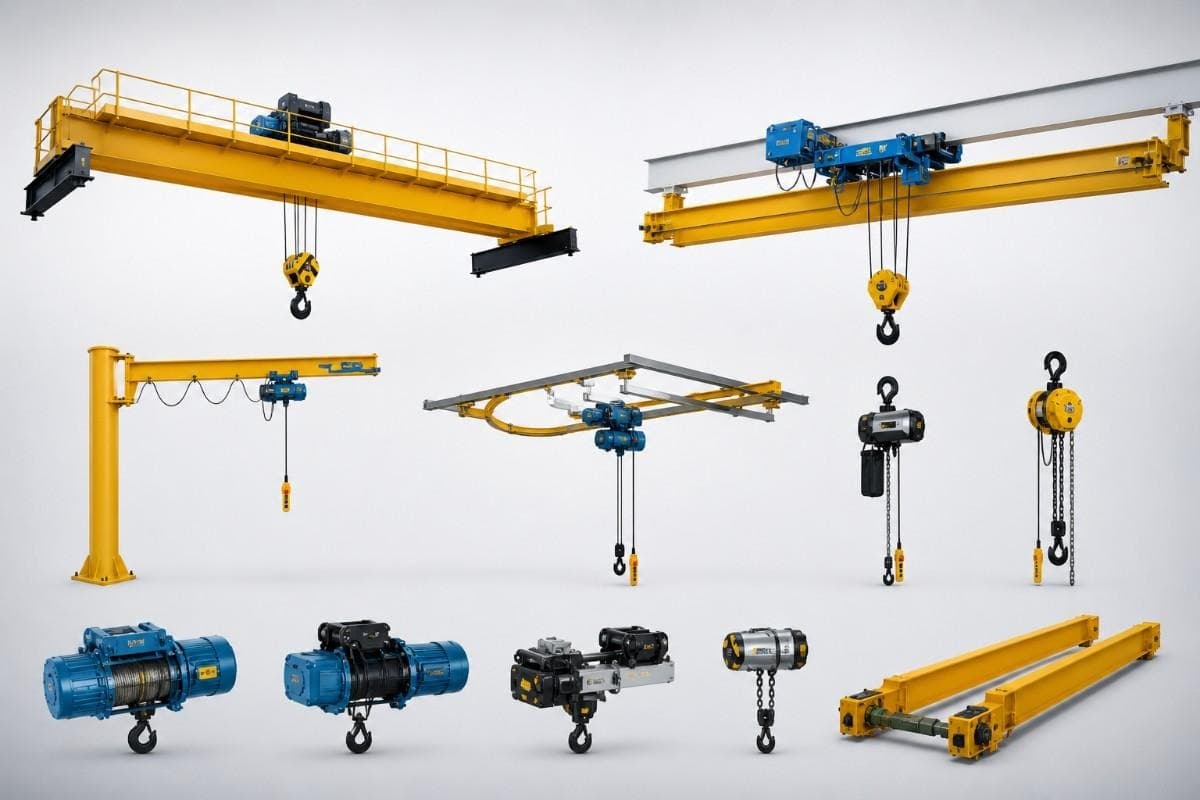
Different industries require different crane designs based on operational needs.
This crane uses one bridge girder and works well for moderate lifting applications.
It’s commonly used in:
Designed with two girders for higher lifting capacity and better load stability.
Ideal for:
The crane travels on rails mounted above runway beams and supports higher capacities.
Mounted below runway beams to maximize vertical workspace.
A crane system works efficiently only when every component performs reliably.
The primary structural beam supporting the crane.
Handles lifting and lowering operations.
Common hoist types include:
Moves the hoist horizontally across the girder.
Allow crane movement along the runway tracks.
Controls crane movement, safety systems, and operational functions.
Not every crane supplier delivers the same engineering quality or support standards.
When I tried evaluating crane systems during a plant modernization project, I realized quickly that technical expertise matters just as much as product specifications.
Manufacturers should understand real industrial operating conditions.
Every facility has different space, load, and operational requirements.
Modern cranes should include:
Strong structural fabrication improves crane lifespan and reliability.
Reliable support services help minimize downtime over the long term.
Overhead cranes support operations across many sectors.
Factories use cranes to move machinery components and raw materials.
Heavy steel coils and fabricated structures require efficient lifting systems.
Assembly lines depend on controlled material movement.
Cranes help improve storage handling and loading efficiency.
Heavy equipment maintenance often requires overhead lifting systems.
At Times Krane, we’ve seen industries improve operational efficiency significantly after installing properly designed overhead cranes tailored to their workflow.
The right crane system changes how a facility operates day to day.
Workers move heavy materials faster and more efficiently.
Overhead systems keep floor areas less congested.
According to the Occupational Safety and Health Administration, reducing manual material handling lowers workplace injury risks considerably.
Crane systems allow controlled movement of large or delicate loads.
Facilities rely less on forklifts and manual lifting equipment.
I’ve noticed that facilities using efficient overhead systems experience smoother production coordination overall.
Here’s why:
Even simple improvements in material handling can create major productivity gains over time.
Safety remains one of the most important aspects of crane operations.
Prevent lifting beyond safe operational limits.
Allow immediate shutdown during unsafe situations.
Prevent excessive crane movement.
Alert workers during crane operation.
Help stabilize suspended loads during movement.
At Times Krane, safety-focused crane engineering remains a priority because industrial lifting environments demand dependable protection systems.
Even high-quality crane systems require proper maintenance to perform consistently.
Inspect:
Lubrication helps reduce wear and friction.
Small issues often become larger operational problems when ignored.
Experienced operators reduce unnecessary strain on crane systems.
In my experience, facilities with preventive maintenance programs usually experience fewer unexpected crane shutdowns.
Selecting a manufacturer involves more than comparing specifications.
Before making a decision, evaluate:
A dependable manufacturer helps ensure long-term crane performance and operational reliability.
At Times Krane, the focus stays on practical lifting solutions designed for real industrial challenges.
Businesses value:
For industries handling continuous production and heavy material movement, working with experienced over head crane manufacturers helps create smoother, safer, and more efficient operations.
Industrial crane systems continue evolving with smarter technologies.
Modern cranes now include:
When I visited a modern manufacturing plant recently, operators were using wireless crane controls to improve handling precision and reduce movement delays significantly.
The future of overhead lifting is becoming more connected, efficient, and safety-focused.
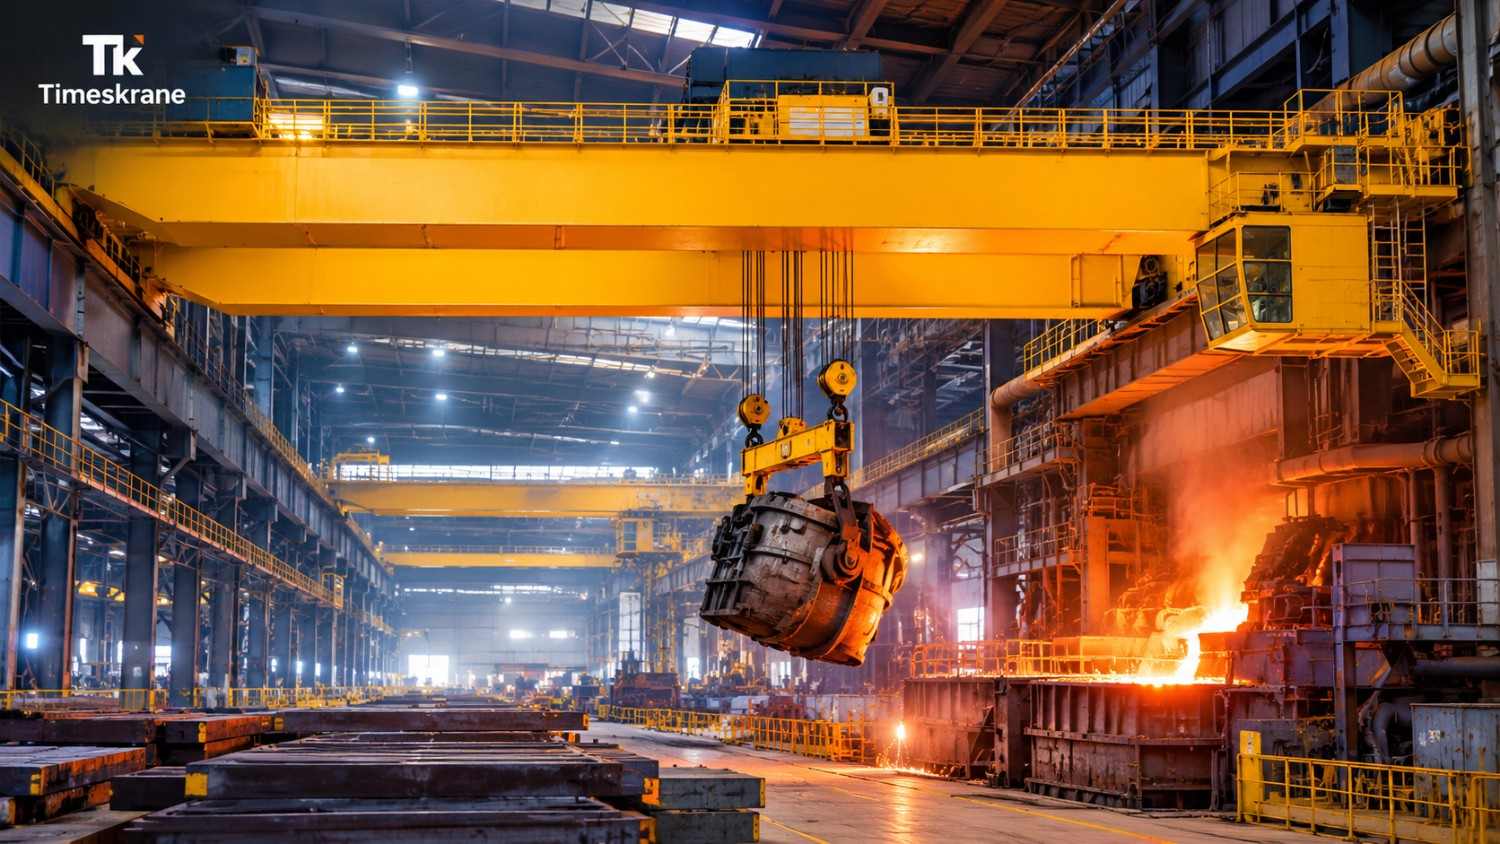
An honest breakdown of what makes a crane genuinely heavy duty for steel plant use, covering duty classification, capacity, and safety features buyers often miss.
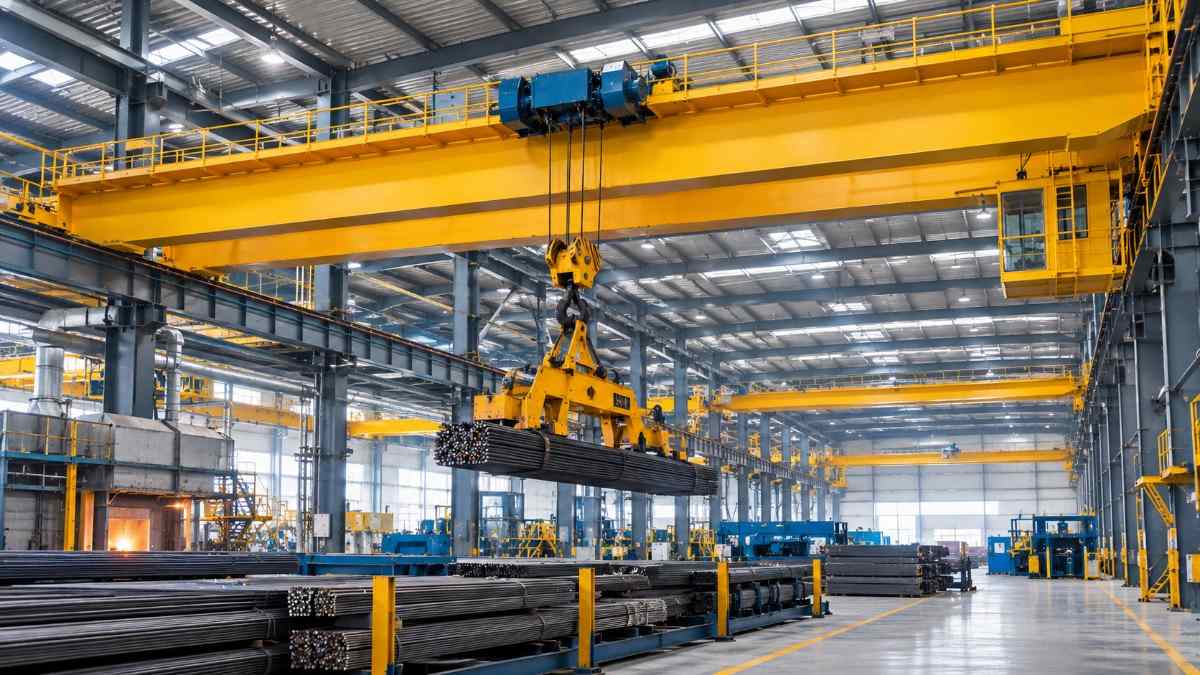
Finding the right steel plant crane manufacturer is perhaps the most important decision a procurement manager or plant owner will make. A poorly designed crane can increase both safety risks and downtime while excessively increasing maintenance costs.
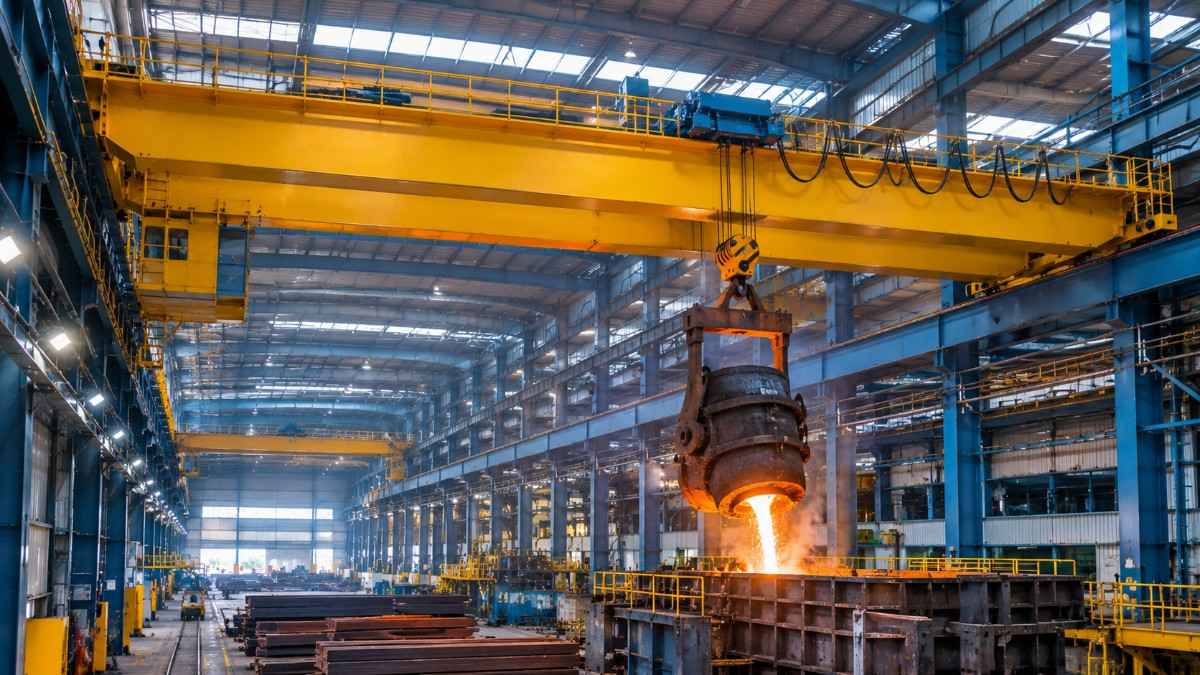
If you run or manage a steel plant, you already know that an overhead crane for steel plant operations is not a luxury. It is the backbone of your material handling process. From moving billets and coils to shifting ladles of molten metal, the right crane decides how smoothly your production line runs.
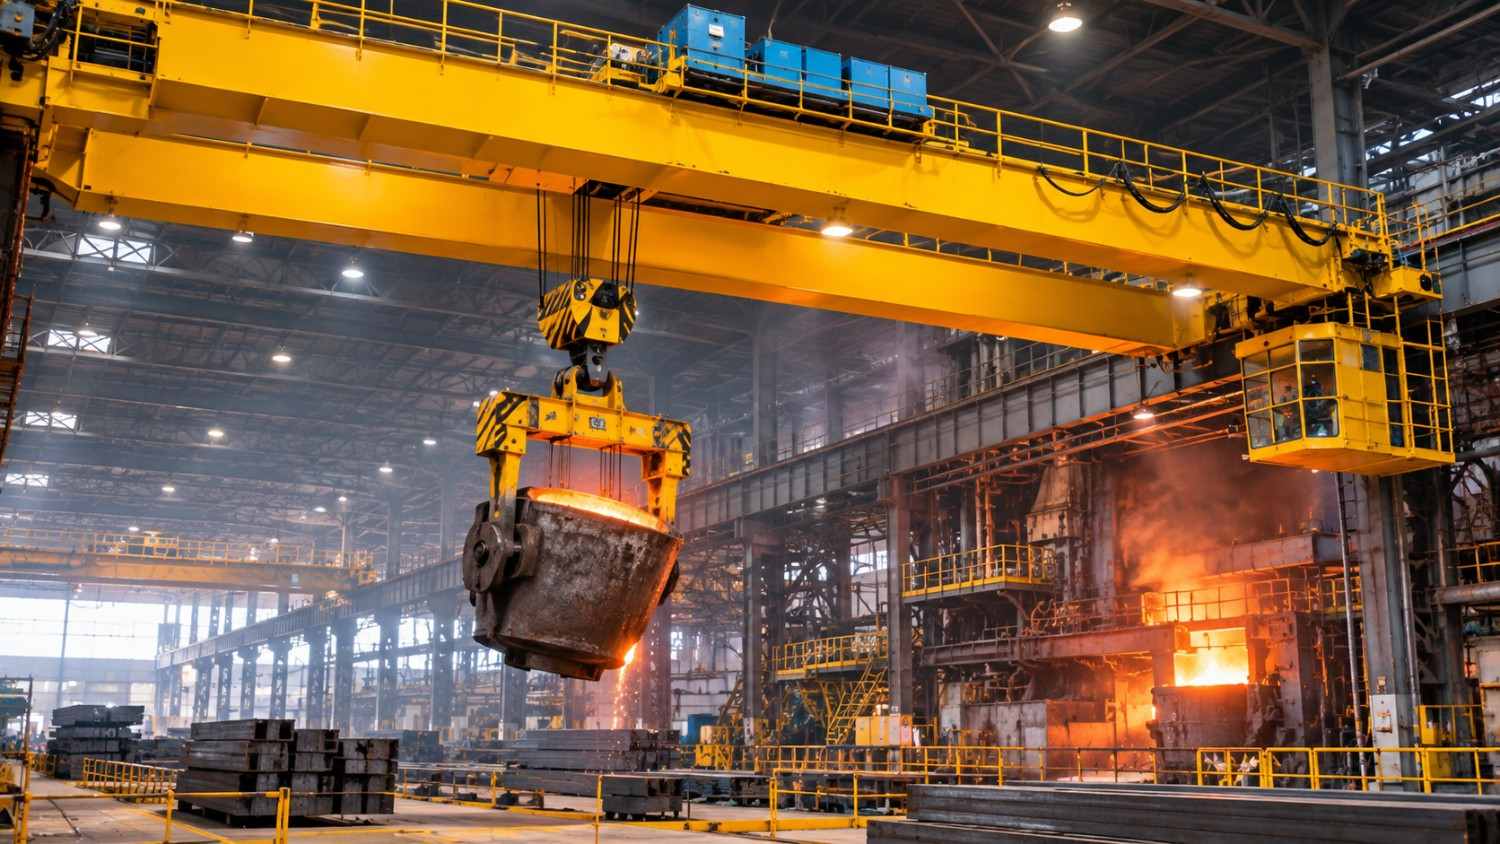
Discover how EOT cranes support steel plant operations, from material handling to molten metal lifting. Learn about crane types, duty classes, safety features, and how to choose the right EOT crane for your steel plant.
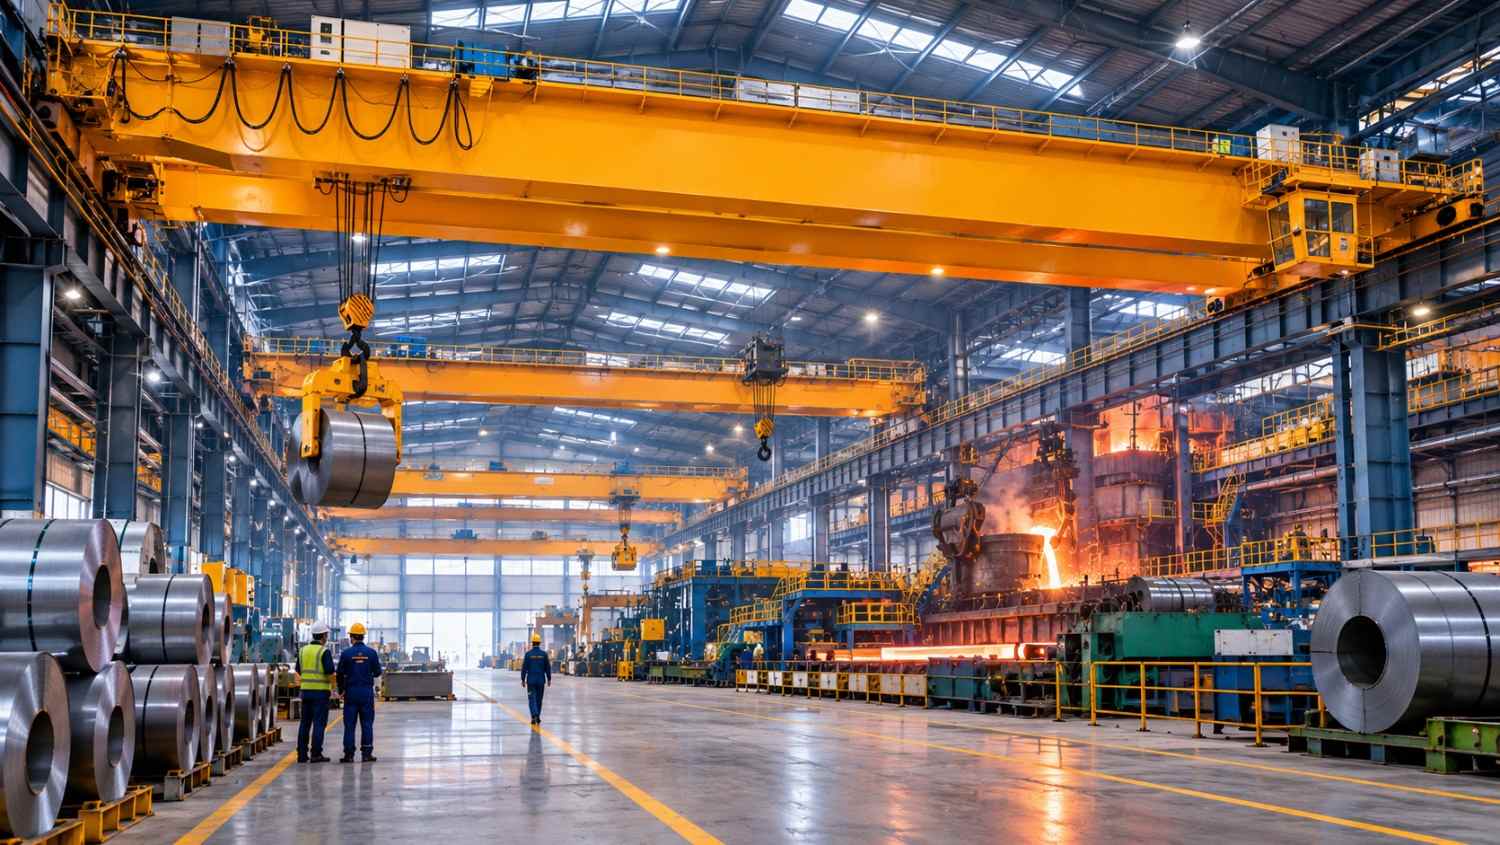
An honest, researched look at the top 5 crane manufacturers for steel plants in India, covering ladle, grab bucket, and coil handling cranes.
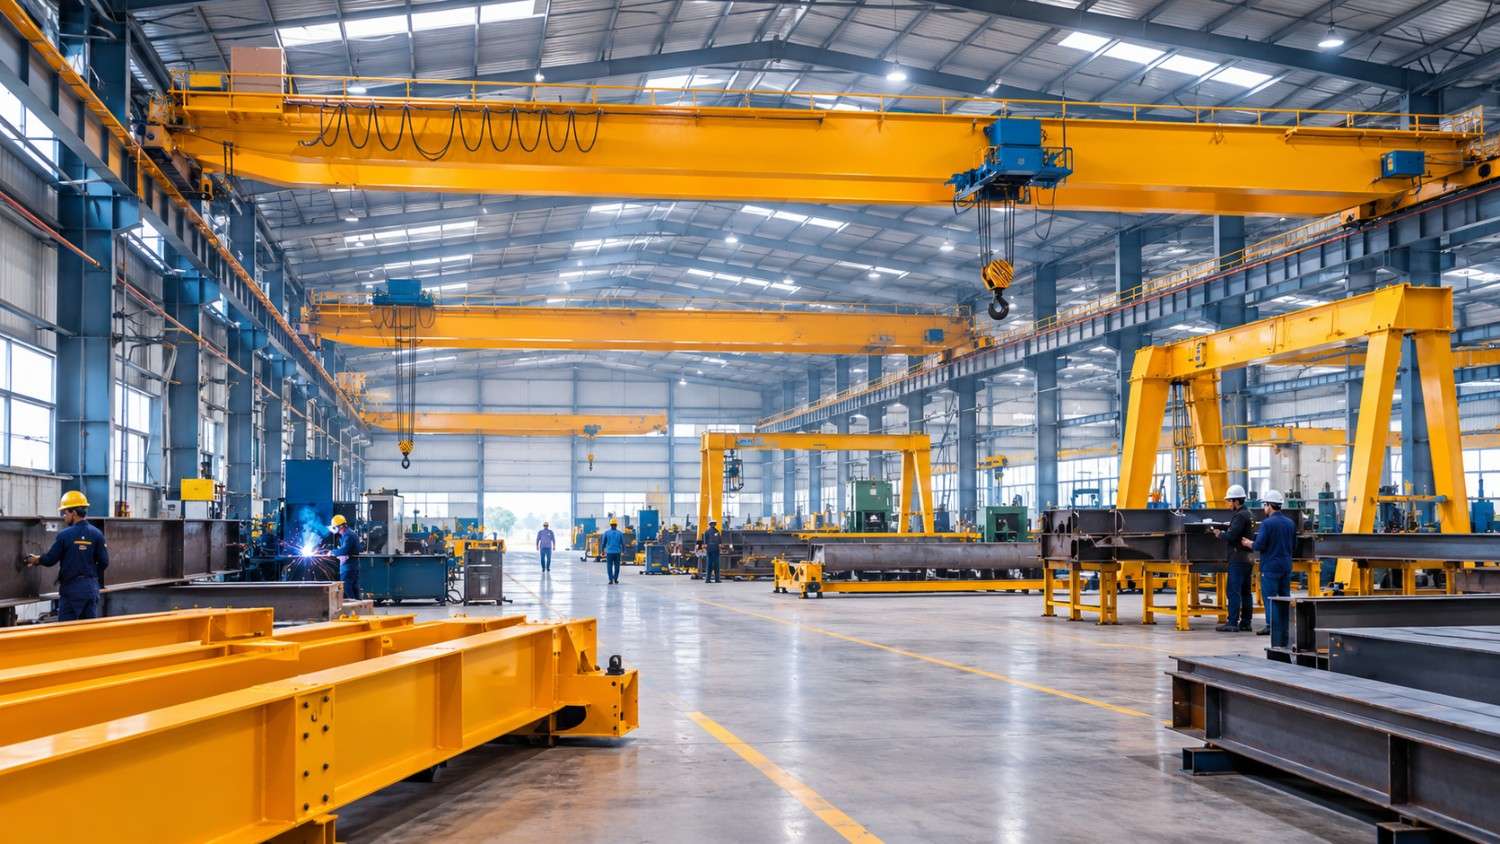
A real, researched look at the top 10 crane manufacturers in North India, covering Delhi NCR, Punjab, Haryana, UP, and Rajasthan, with what actually sets each one apart.
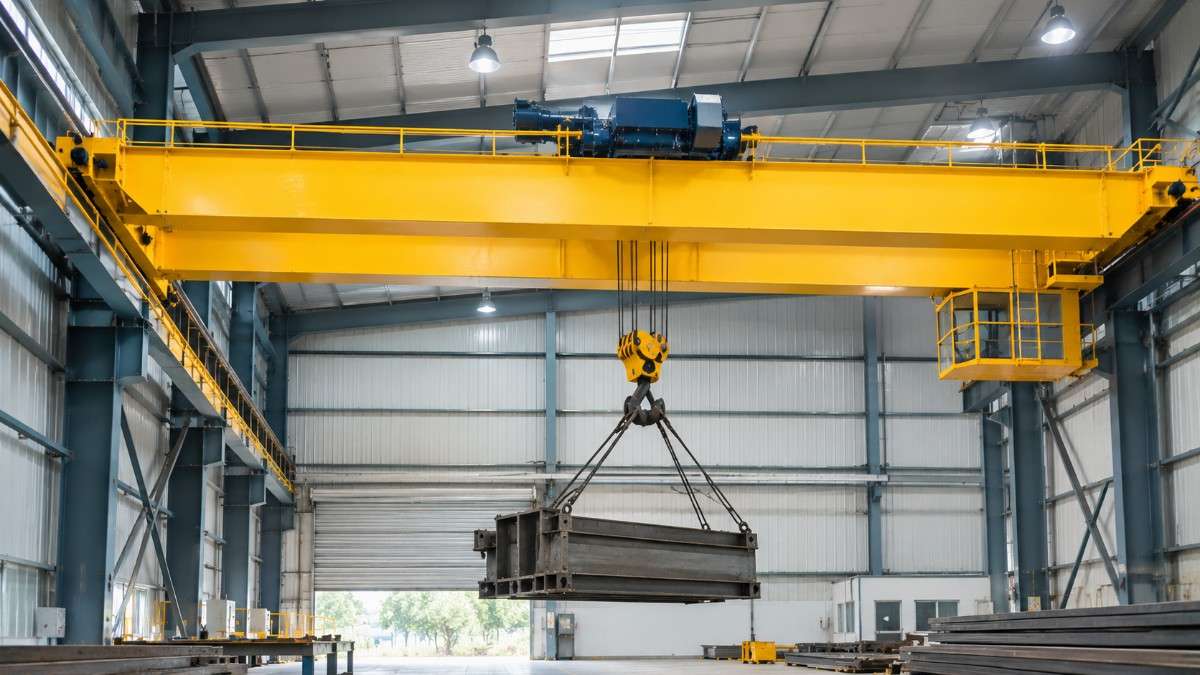
If you are looking for a 10 ton overhead crane for your factory or warehouse, the primary question that arises in your mind is whether this capacity will cater to your daily operations or it will turn out to be a useless and bulky addition to your storage.
Looking for a reliable partner for your next industrial project?