English
Contact
Configure
Catalog
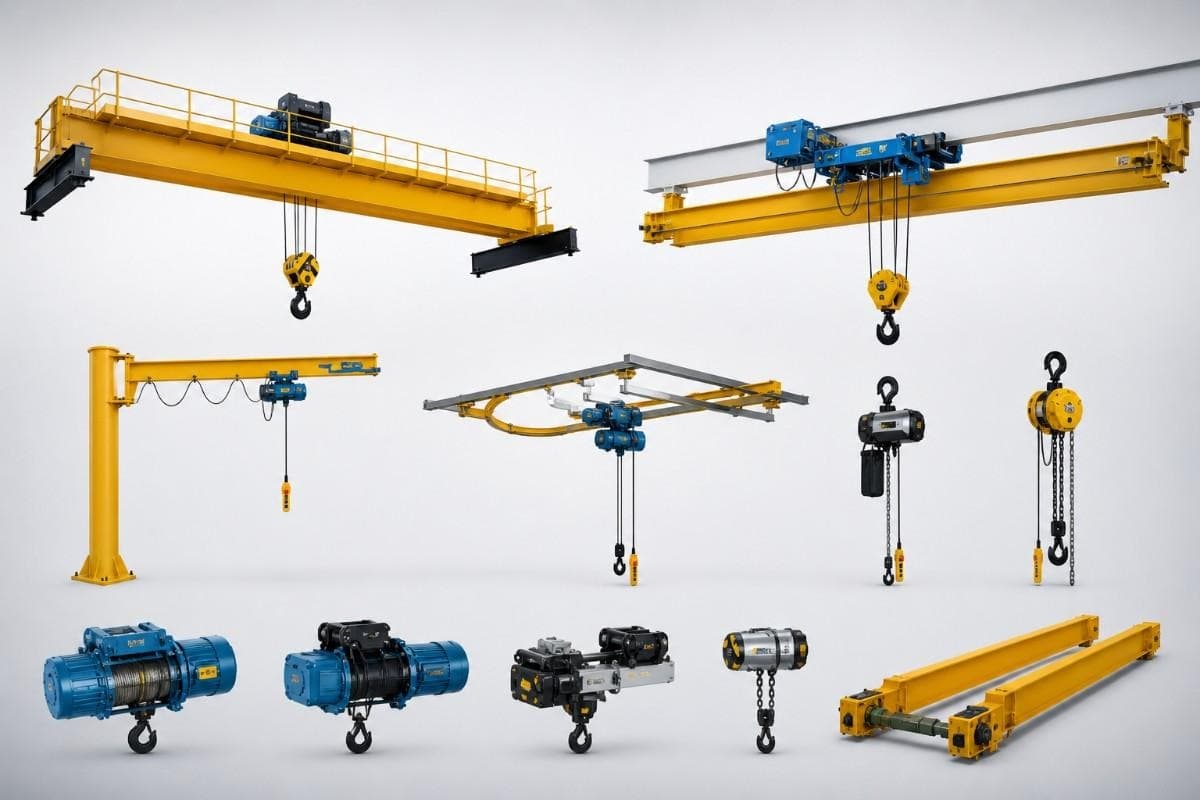
That’s why experienced gantry crane manufacturers play such an important role across industries handling heavy materials every day.
A well-engineered gantry crane improves workflow efficiency, enhances workplace safety, and provides flexible lifting support in areas where traditional overhead cranes may not be practical.
At Times Krane, we’ve worked with industries where reliable lifting systems directly affect operational timelines. In many cases, gantry cranes become the preferred solution because they offer both mobility and strength without requiring complex building support structures.
A gantry crane is a material handling system supported by legs that travel on wheels or rails installed on the ground.
Unlike overhead cranes mounted directly onto building structures, gantry cranes are more flexible and can operate across open spaces, outdoor yards, and large industrial facilities.
A typical gantry crane includes:
You’ll commonly see gantry cranes in:
Efficient material movement keeps industries productive. When heavy loads move smoothly, operations stay organized and downtime reduces significantly.
I’ve noticed that businesses handling oversized materials often prefer gantry cranes because they provide lifting flexibility without depending entirely on permanent structural supports.
Reliable gantry crane manufacturers help industries improve:
Different industrial applications require different crane designs.
This crane uses two supporting legs running on rails installed at floor level.
Commonly used in:
One side operates on ground rails while the opposite side moves on elevated runway beams.
Designed for smaller operations requiring mobility and easy relocation.
Suitable for moderate lifting applications and lighter operational requirements.
Built for heavy-duty lifting with enhanced stability and higher load capacity.
Every crane system depends on several carefully engineered parts working together.
The primary horizontal beam supporting the trolley and hoist system.
Handles lifting and lowering operations.
Common hoist types include:
Provide structural balance and crane support.
Moves the hoist horizontally across the bridge girder.
Allow crane movement along rails or operating surfaces.
Controls crane movement, safety systems, and operational functions.
Not every crane system performs reliably under continuous industrial pressure. Engineering quality matters more than many buyers initially realize.
When I tried reviewing lifting systems during a fabrication plant expansion, I quickly noticed that crane durability depends heavily on structural design and component quality.
Gantry cranes work efficiently in both indoor and outdoor environments.
Unlike fixed overhead cranes, gantry systems require less building infrastructure.
Large materials can move across wide operational areas smoothly.
Overhead lifting reduces congestion at floor level.
These cranes are designed to handle large and bulky materials safely.
Gantry cranes support operations across multiple industrial sectors.
Used for moving construction materials and heavy equipment.
Steel plates, fabricated structures, and coils require strong lifting systems.
Warehouses use gantry cranes for organized material movement.
Factories rely on cranes for machine handling and production support.
Container handling operations commonly depend on gantry crane systems.
At Times Krane, we’ve seen how properly engineered gantry cranes improve workflow efficiency in industries where heavy material movement is a daily requirement.
One thing I’ve noticed in large industrial yards is how quickly operations slow down when material movement depends entirely on forklifts or manual coordination.
Gantry cranes help solve many of these operational bottlenecks.
Here’s how they improve productivity:
Even small improvements in lifting efficiency can create significant productivity gains over time.
Choosing the right manufacturer involves more than comparing technical specifications.
Manufacturers should understand real industrial operating conditions.
Every industry has different lifting and layout requirements.
Modern gantry cranes should include:
High-quality fabrication improves crane lifespan and reliability.
Reliable support services help reduce downtime and maintenance issues.
Safety remains one of the most important aspects of crane operations.
Prevent lifting beyond safe capacity limits.
Allow immediate crane shutdown during emergencies.
Alert workers during crane movement.
Helps stabilize suspended loads during travel.
Prevent unsafe operational movement.
According to a report from the Material Handling Industry Association, facilities using advanced safety-equipped crane systems reported noticeable improvements in operational safety and reduced workplace incidents.
Even high-quality cranes require regular maintenance for reliable performance.
Inspect:
Lubrication helps reduce wear and mechanical strain.
Ignoring small issues often leads to larger breakdowns later.
Skilled operators help extend equipment lifespan significantly.
In my experience, facilities following preventive maintenance programs usually experience fewer unexpected crane shutdowns.
Before selecting a gantry crane, evaluate:
I’ve noticed that businesses planning for long-term expansion usually make more effective crane investments compared to those focusing only on immediate requirements.
At Times Krane, the focus remains on delivering durable lifting systems designed around practical industrial needs.
Businesses value:
For industries handling demanding material movement operations, working with experienced gantry crane manufacturers helps improve safety, productivity, and long-term operational efficiency.
Industrial crane systems continue evolving rapidly.
Modern gantry cranes now include:
When I visited a large industrial facility recently, operators were relying heavily on remote-controlled gantry cranes because they improved handling precision and reduced operational delays considerably.
The future of industrial lifting is becoming smarter, safer, and more efficient.
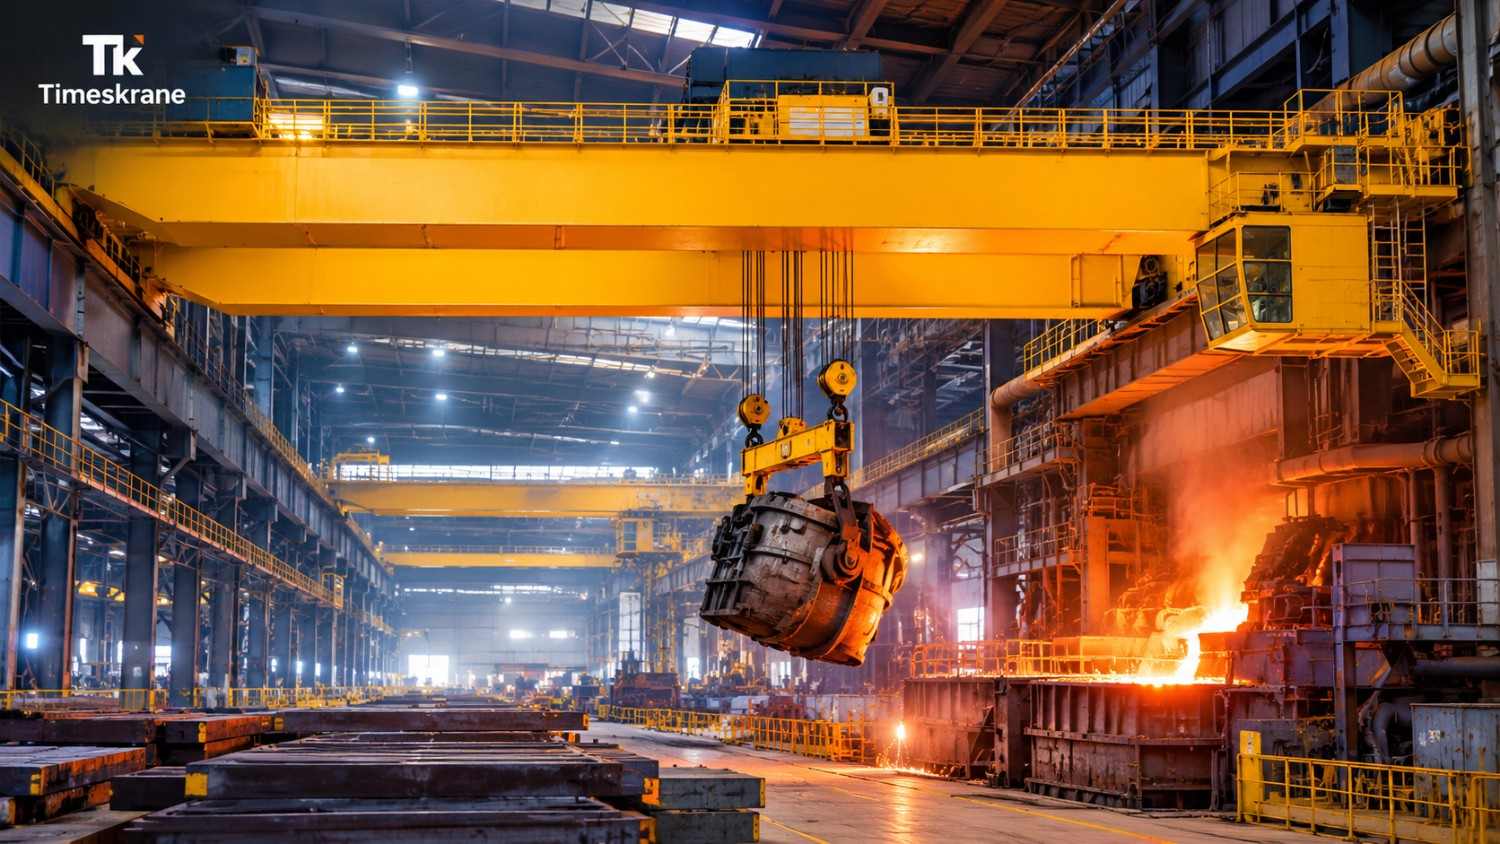
An honest breakdown of what makes a crane genuinely heavy duty for steel plant use, covering duty classification, capacity, and safety features buyers often miss.
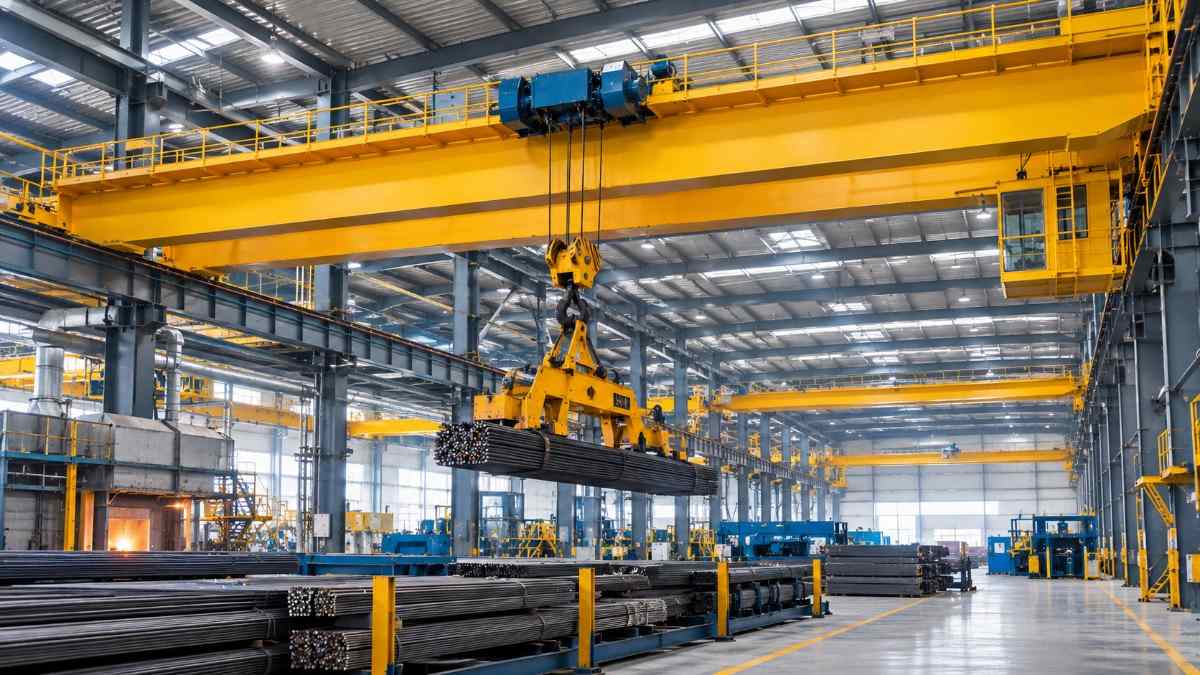
Finding the right steel plant crane manufacturer is perhaps the most important decision a procurement manager or plant owner will make. A poorly designed crane can increase both safety risks and downtime while excessively increasing maintenance costs.
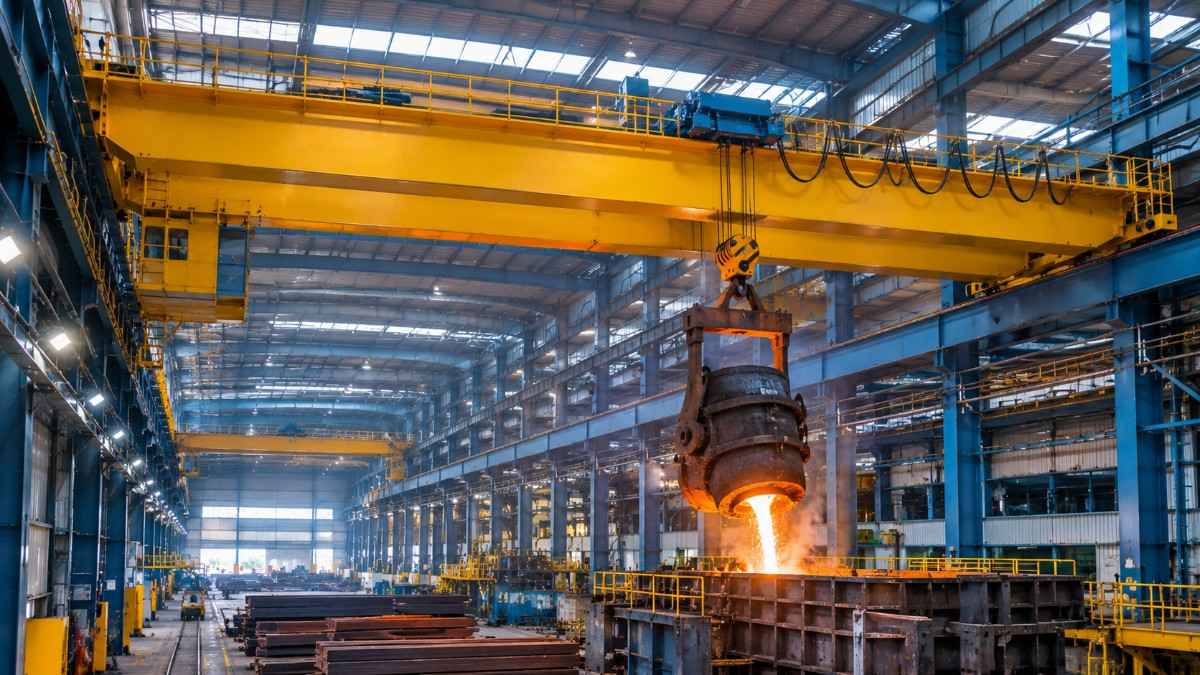
If you run or manage a steel plant, you already know that an overhead crane for steel plant operations is not a luxury. It is the backbone of your material handling process. From moving billets and coils to shifting ladles of molten metal, the right crane decides how smoothly your production line runs.
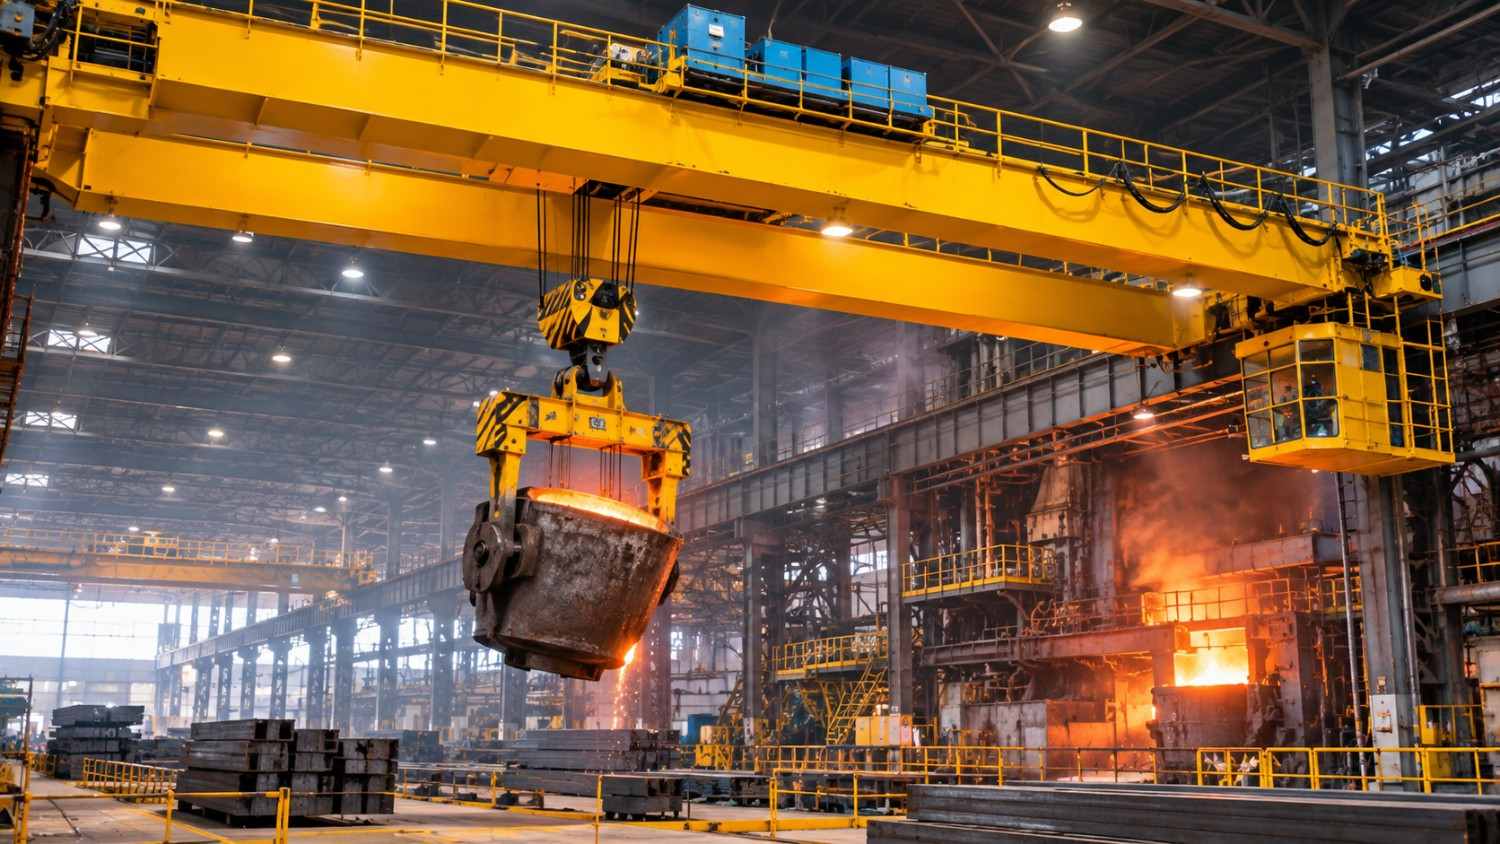
Discover how EOT cranes support steel plant operations, from material handling to molten metal lifting. Learn about crane types, duty classes, safety features, and how to choose the right EOT crane for your steel plant.
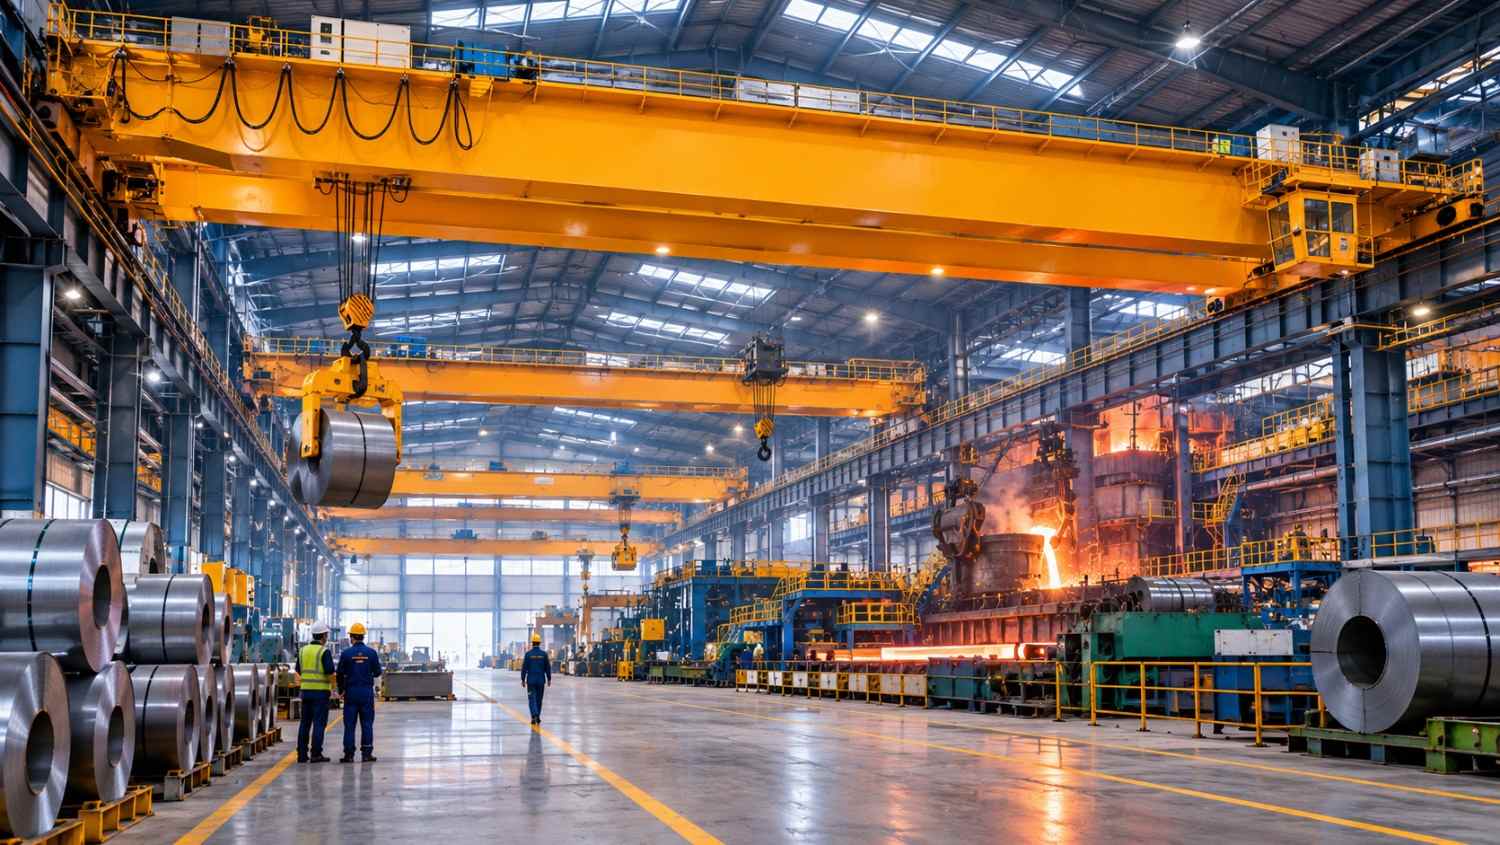
An honest, researched look at the top 5 crane manufacturers for steel plants in India, covering ladle, grab bucket, and coil handling cranes.
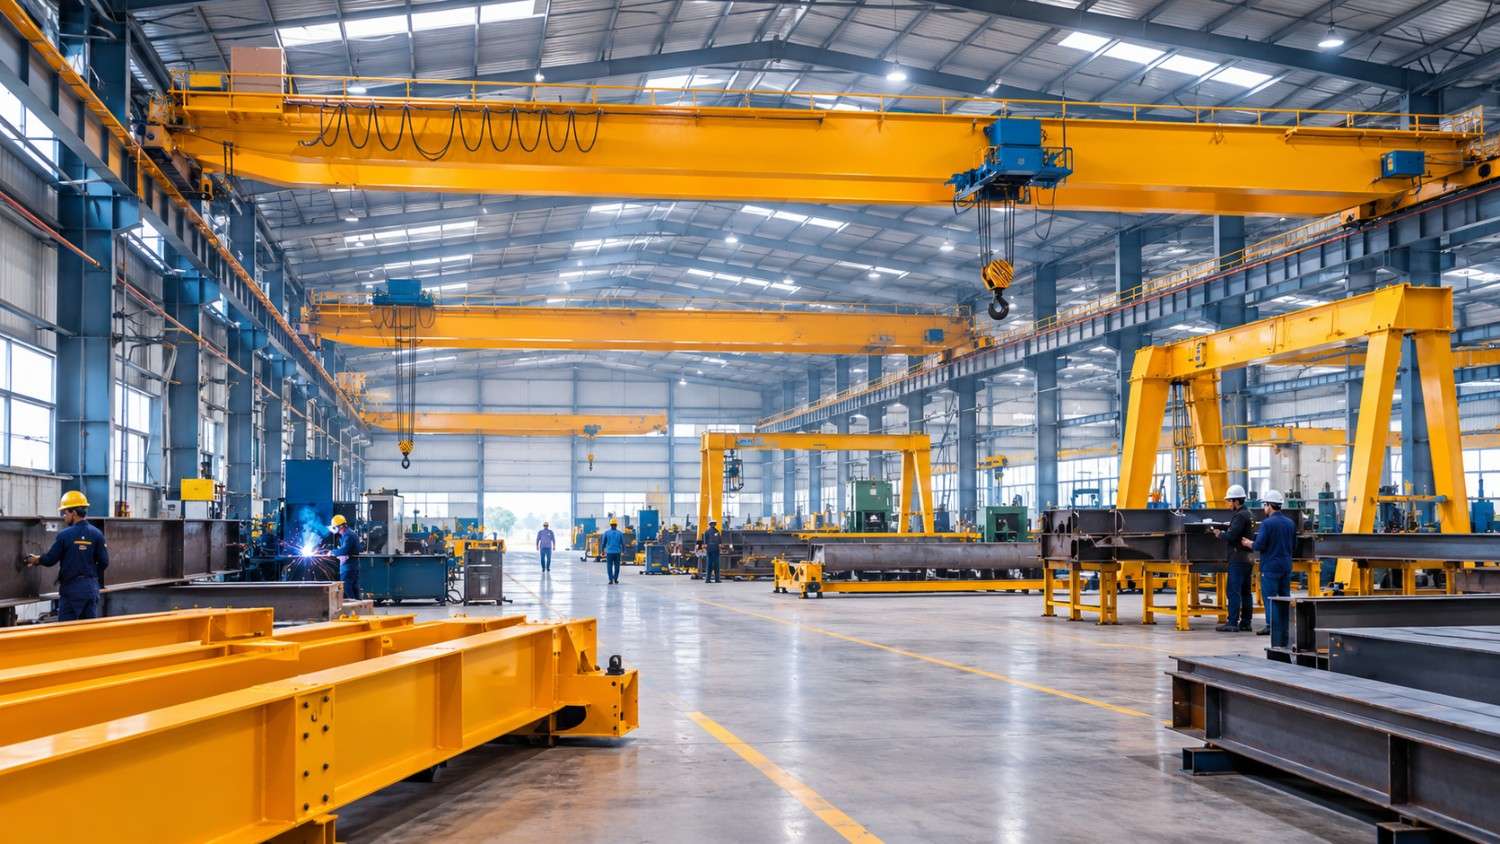
A real, researched look at the top 10 crane manufacturers in North India, covering Delhi NCR, Punjab, Haryana, UP, and Rajasthan, with what actually sets each one apart.
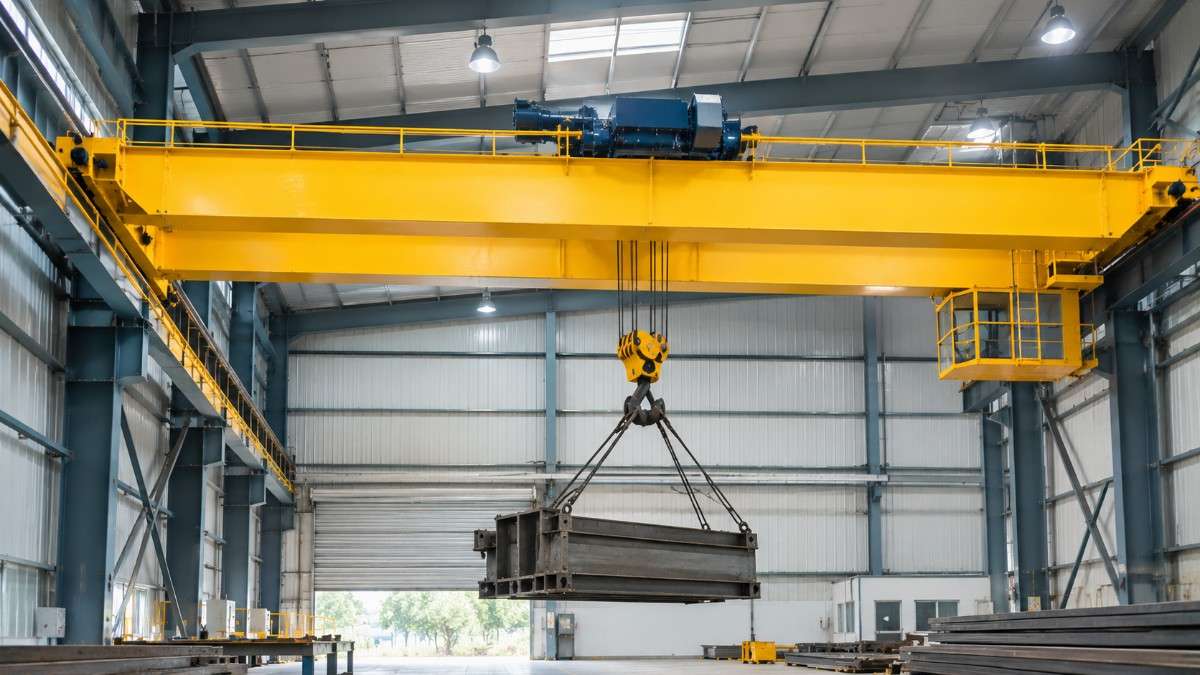
If you are looking for a 10 ton overhead crane for your factory or warehouse, the primary question that arises in your mind is whether this capacity will cater to your daily operations or it will turn out to be a useless and bulky addition to your storage.
Looking for a reliable partner for your next industrial project?